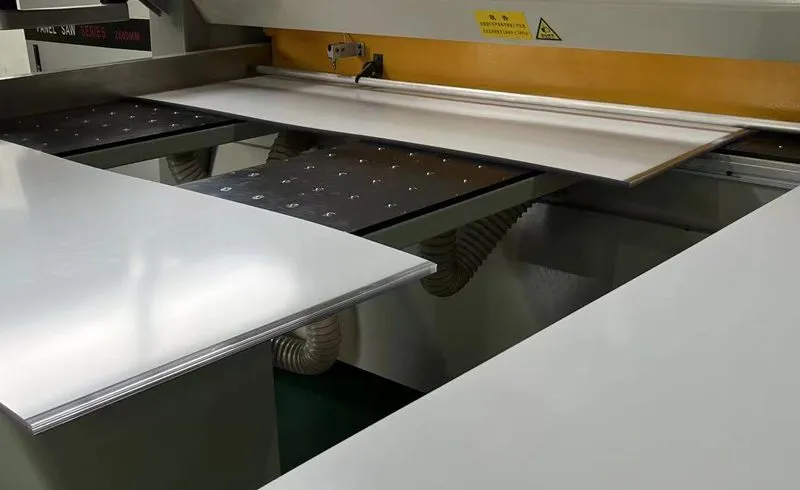
For a clean PC cut, support the sheet, use a sharp plastic-cutting blade and keep chips moving away from the edge. Choose the saw or router from the sheet form, thickness, geometry and required finish. Before production, cut a representative piece and inspect both faces, the exit edge and any holes. A generic RPM copied from another material is not a process approval.
Send a cut-panel drawing See SinoPlastix cut-to-size service
Pick a method from the part, not a one-size-fits-all tool
| Cutting job | Practical route | First thing to check |
|---|---|---|
| Long straight cut in solid PC | Supported circular or panel saw with a sharp carbide-tipped blade intended for plastics; keep masking on. | Clamping, blade condition and chip evacuation; inspect exit-edge chipping and heat marks. |
| Curve or cutout | Jigsaw for short curves or CNC router when repeatable geometry/tolerance matters. | Vibration, minimum radius, hold-down, corner stress and the cut edge after the first pass. |
| Multiwall PC | Fine-toothed saw or approved sheet-specific method with the flutes supported. | Remove swarf from channels, protect the UV face and follow the product’s end-closure instructions. |
| Coated or flame-retardant PC | Check the actual grade’s fabrication guide and trial scrap from the production lot. | Coating damage, edge cracking and any grade-specific restrictions before approving the drawing. |
One named manufacturer’s tool data: a starting reference
The POLYVANTIS LEXAN sheet fabrication guide recommends secure clamping, fine-tooth tools, masking during cutting and chip removal. Its table gives 9–15 mm tooth spacing and 1,800–2,400 m/min for a circular saw, and 1.5–4 mm tooth spacing and 600–1,000 m/min for a band saw. Its jig-saw section cites 2–2.5 mm tooth spacing with low feed. The guide also favours a band saw or jig saw over a circular saw for a single sheet thinner than 3 mm.
These are published settings for named LEXAN sheet products, not SinoPlastix production settings. The source table labels a column “Rotation Speed” but gives m/min, not spindle rpm; confirm the intended cutting-speed interpretation with the tool and grade supplier. Do not enter those numbers directly into a CNC control. Select blade diameter, tooth form, feed, hold-down and grade together, then approve a first article. For multiwall PC, the same manufacturer’s THERMOCLEAR guide calls for supported cutting and removal of sawdust from the channels with dry compressed air.
Diagnose the edge before repeating the cut
| What you see | Likely process questions | First response |
|---|---|---|
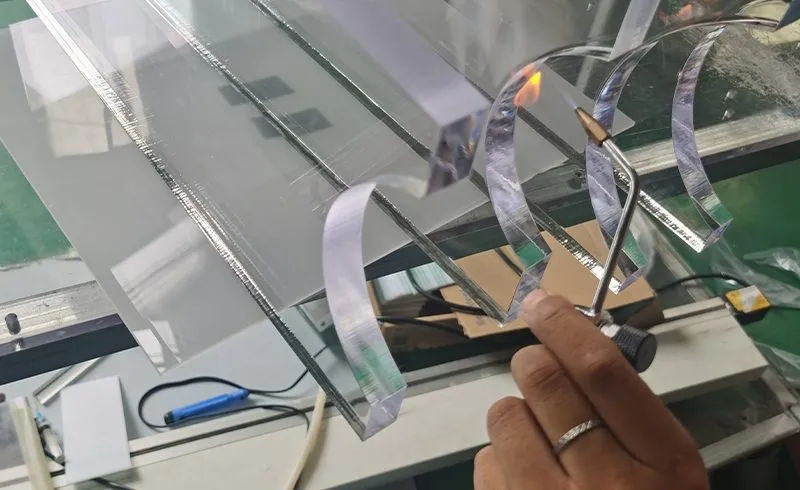
| Glossy, re-welded or melted edge | Rubbing, poor chip escape, dull tooth, excessive heat? | Stop the run; inspect the tool and evacuation, then repeat on scrap with a controlled feed. |
| Chipped exit, white stress line or fine crack | Sheet vibration, unsupported exit, tooth geometry, local pressure? | Improve support and hold-down, inspect the blade and repeat the first article. |
| Swarf caught inside multiwall channels | Was the flute direction supported and cleaned before closure? | Clean according to the offered sheet guide before sealing the ends; do not hide chips behind tape. |
Deburring, sanding and polishing are separate finishing decisions. A visually clear edge does not prove suitability for later bonding, bending or a loaded safety component. Identify that later process on the drawing before accepting the cut.
Approve a first article, then quote the repeat run
- Confirm the PC grade, thickness, sheet type, UV/coated face, masking and tolerance.
- Cut the longest edge, tightest radius and most difficult exit on order-representative stock.
- Inspect both faces, edge, holes and protective film under useful light; record actual cut settings, tool ID, support and operator sign-off.
- Repeat enough pieces to see whether tool wear changes the result; agree which defects are acceptable before full production.
SinoPlastix has 22 CNC machines and can quote custom cut PC parts from your drawing. The written quotation sets the actual grade, edge finish, quantity, price and lead time; project complexity affects lead time.
Copy a cutting brief into your inquiry
Fill these lines and paste them into the RFQ message; upload a drawing if you have one.
Request cut PC panels Review CNC machining capability
Common questions
Can I cut polycarbonate with a circular saw?
Yes, for a suitable grade and sheet thickness, with full support, a sharp plastic-cutting blade, masking and controlled chip removal. Trial the actual stock and inspect the edge before production.
Can I score and snap PC sheet?
Do not assume so. It depends on the thin-sheet grade and its manufacturer’s instructions; for many production cuts, a supported saw or router provides a more controlled result.
Is a polished cut edge ready for bonding?
Not automatically. Cutting and finishing can leave stress or contamination. Specify the subsequent joining method and approve a representative test with the offered PC grade.